Food Packaging Machine Supplier Solutions

All Categories

food packaging machine supplier

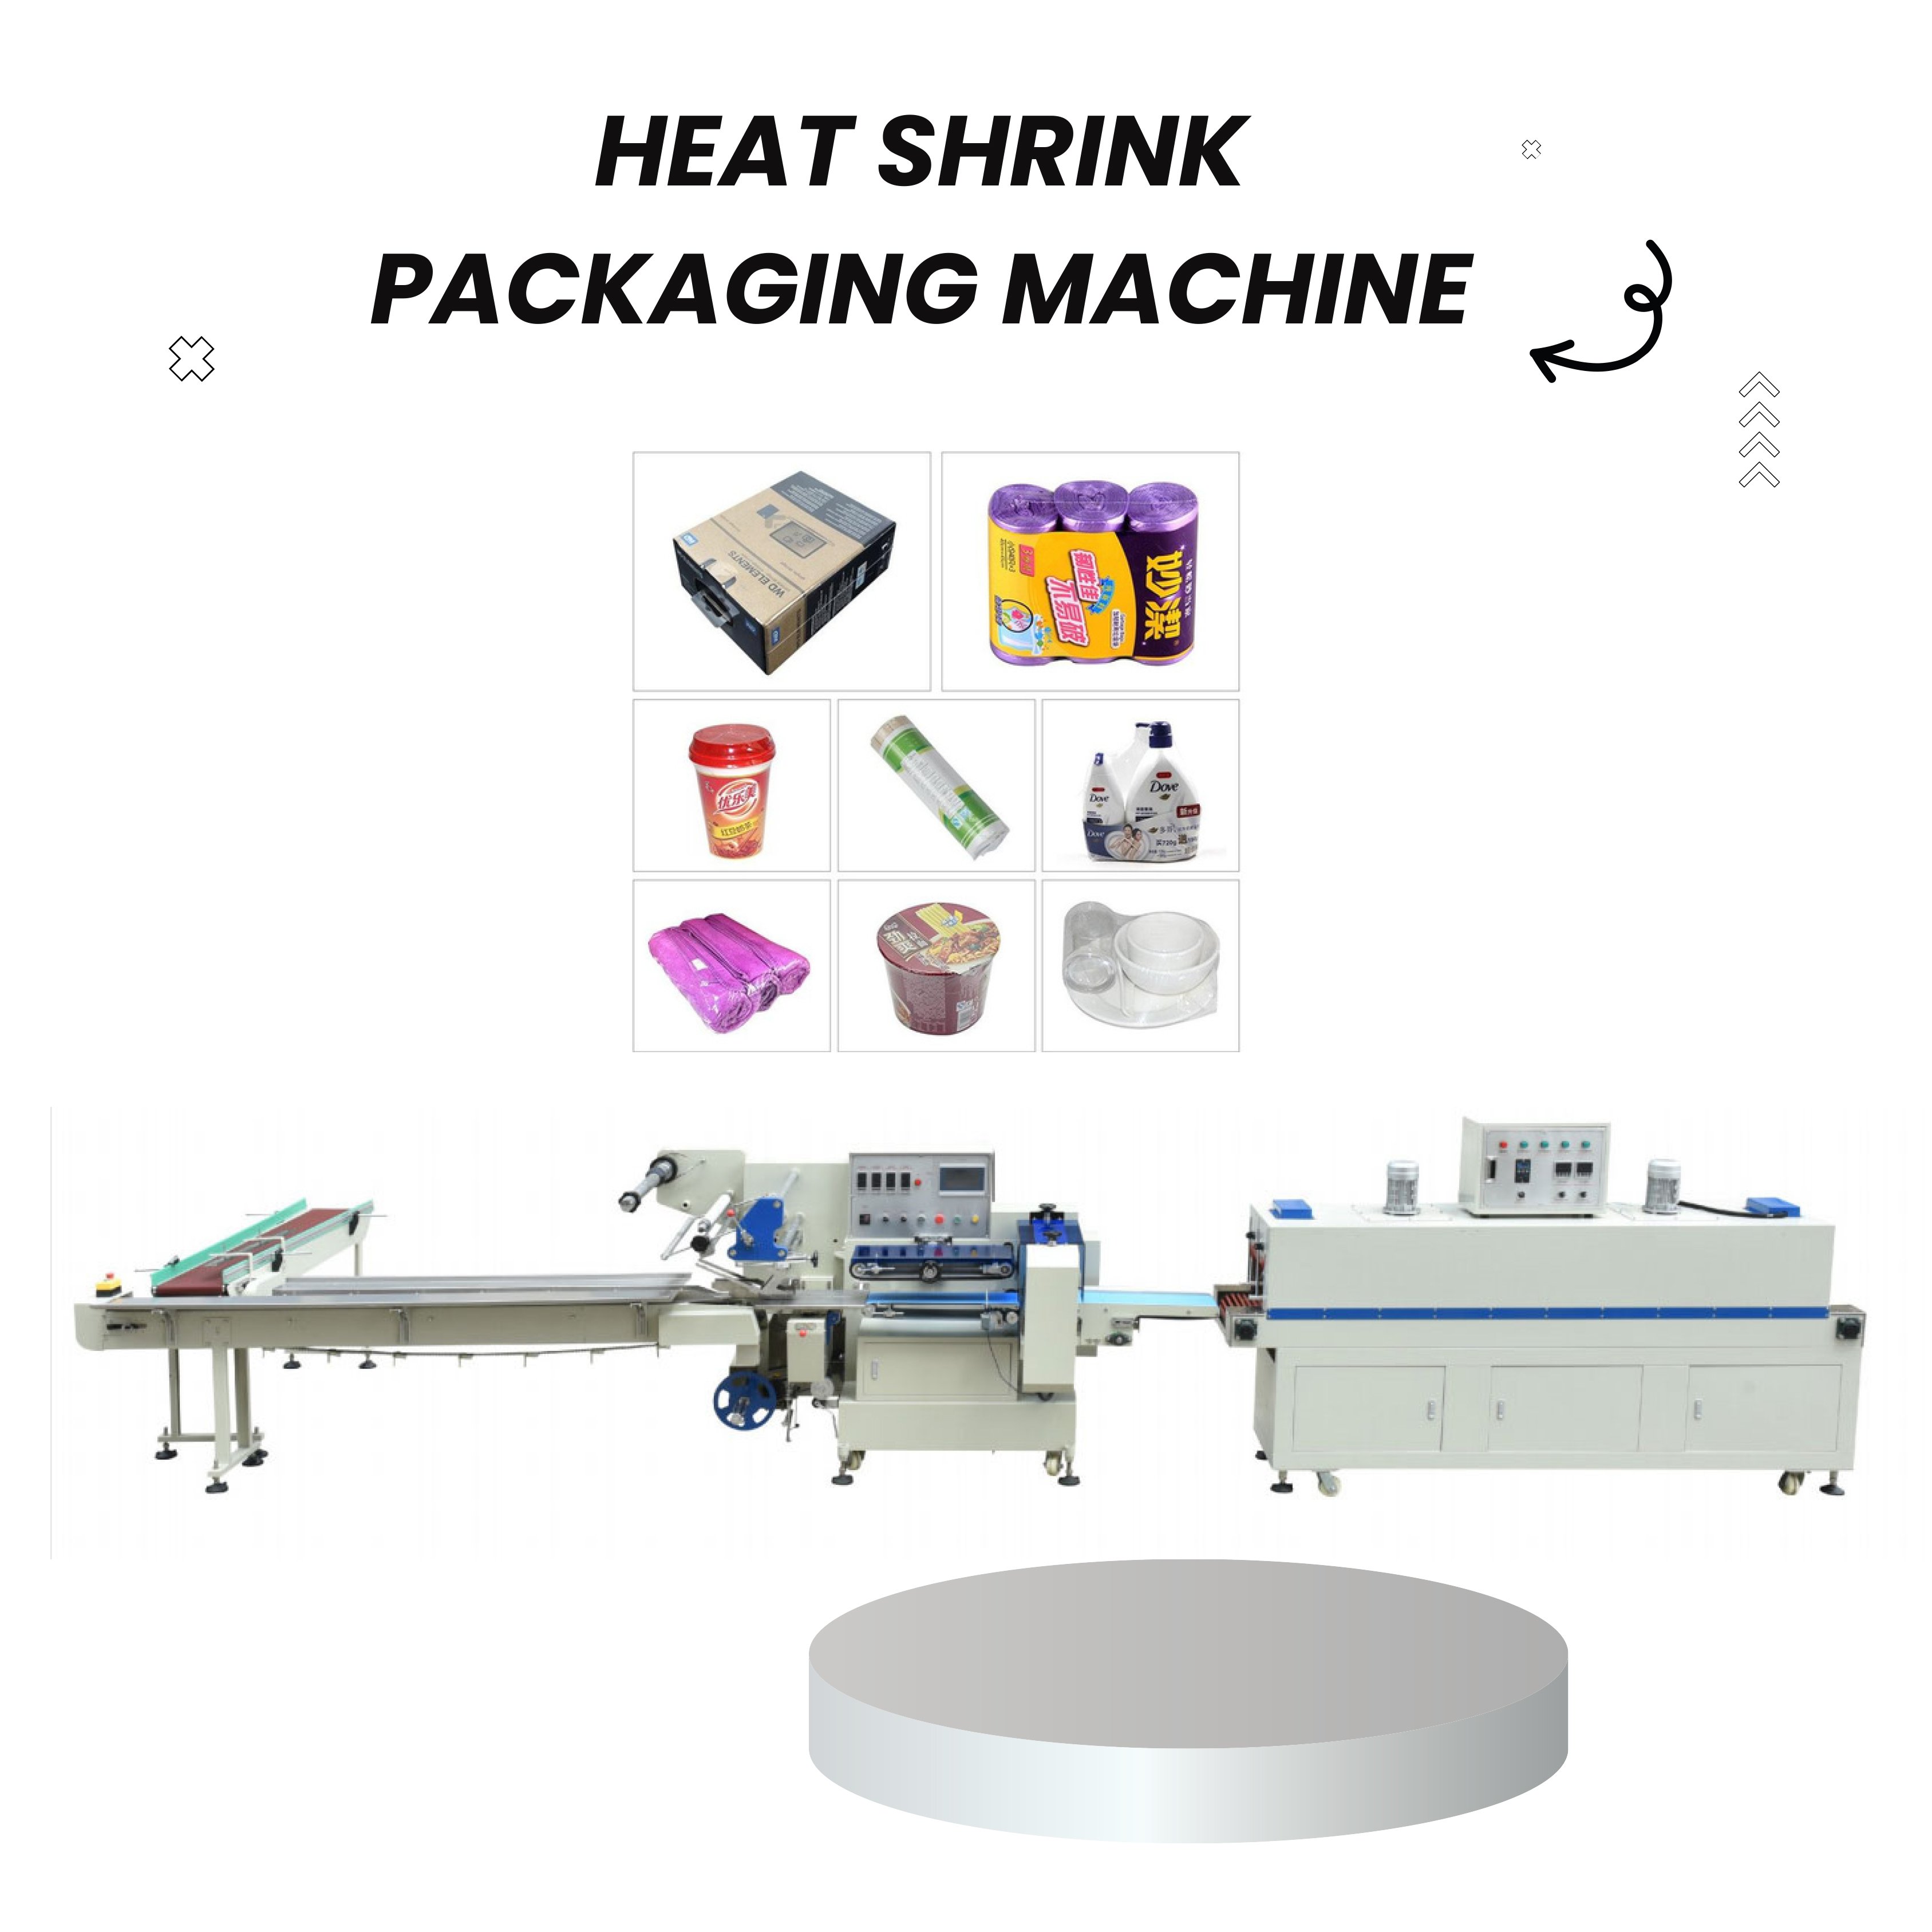
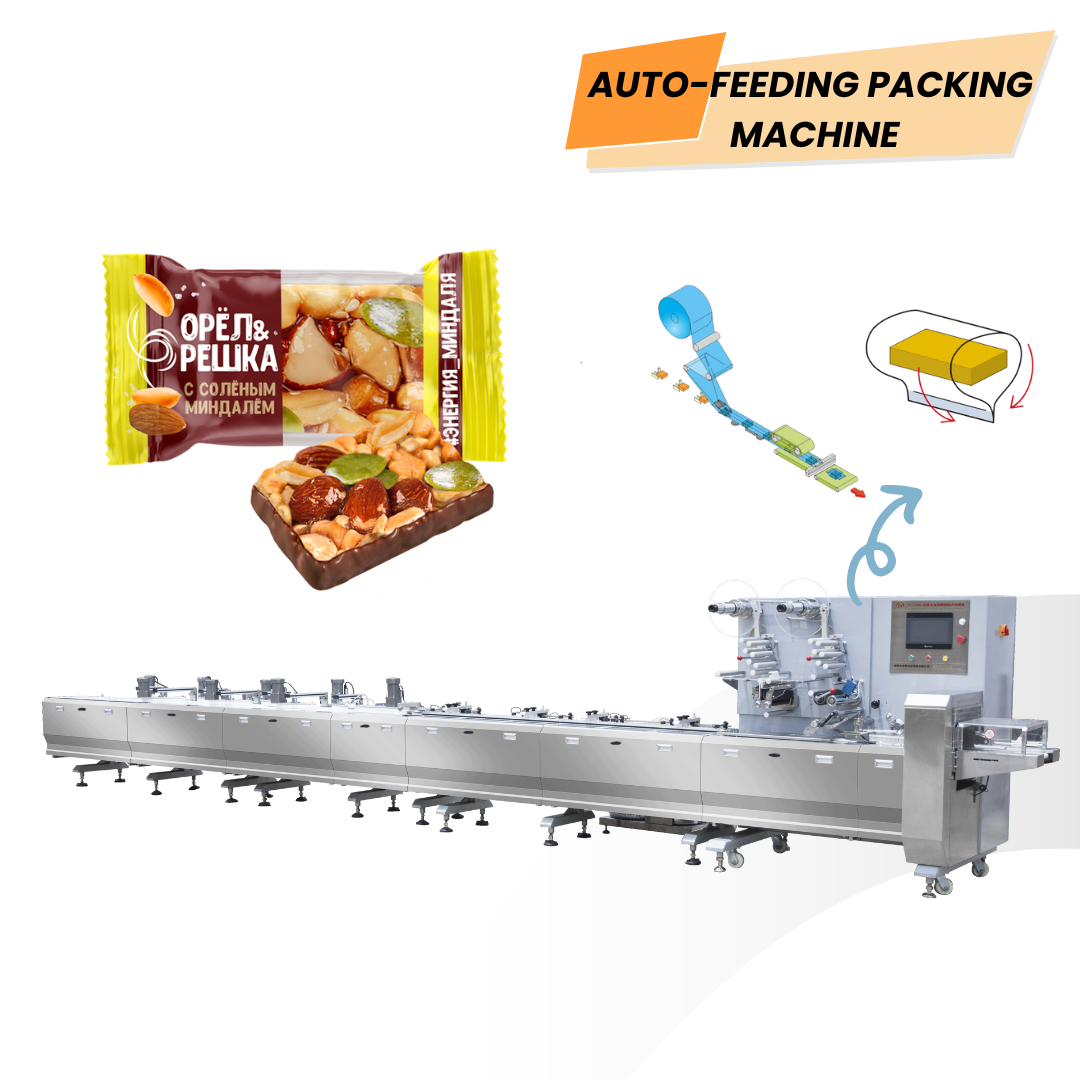
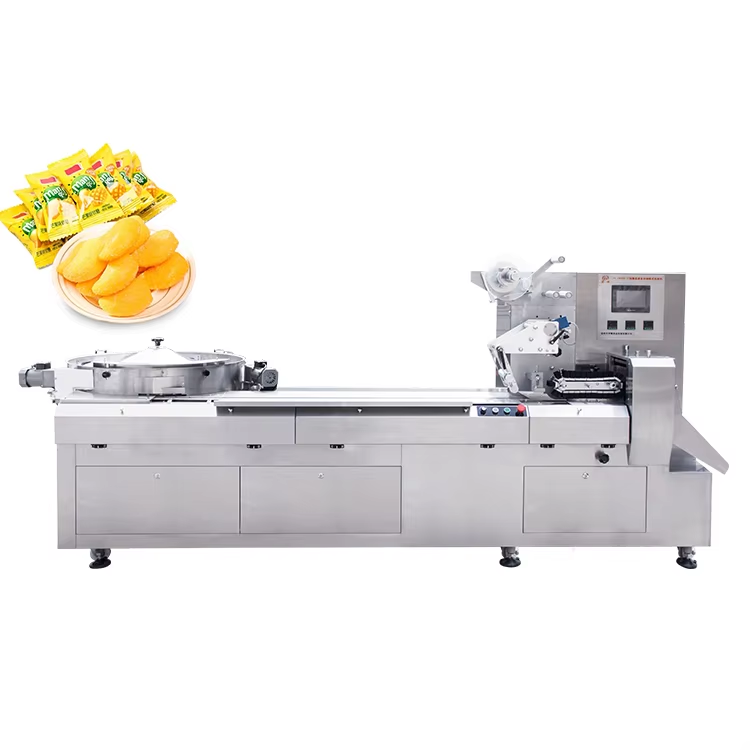
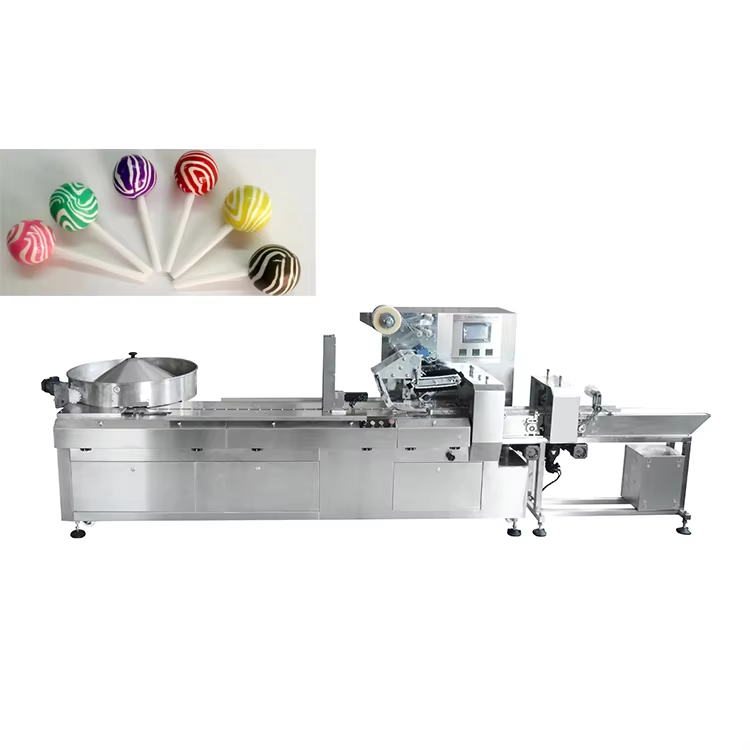
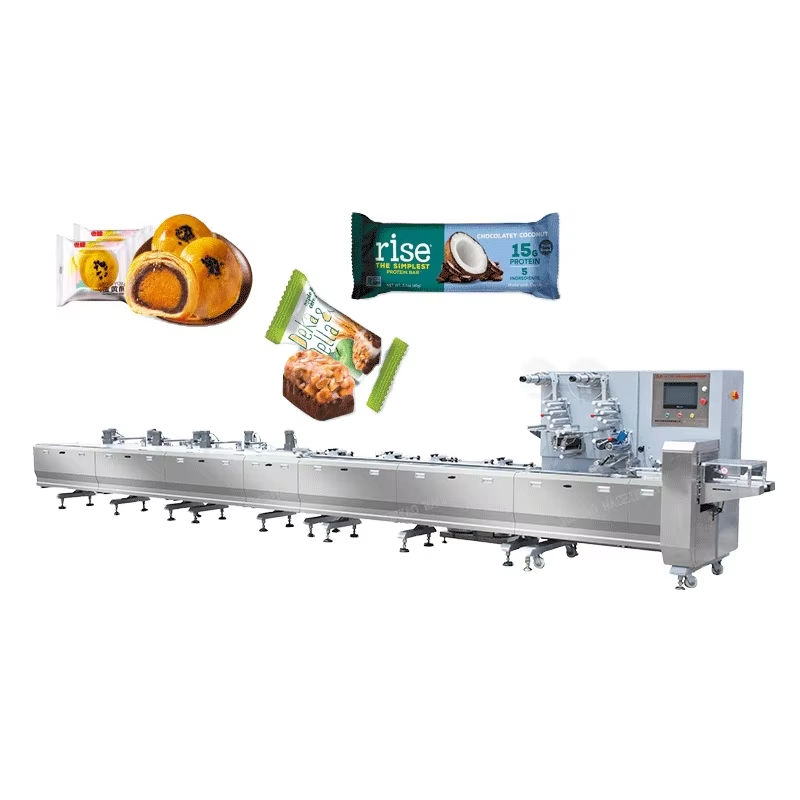
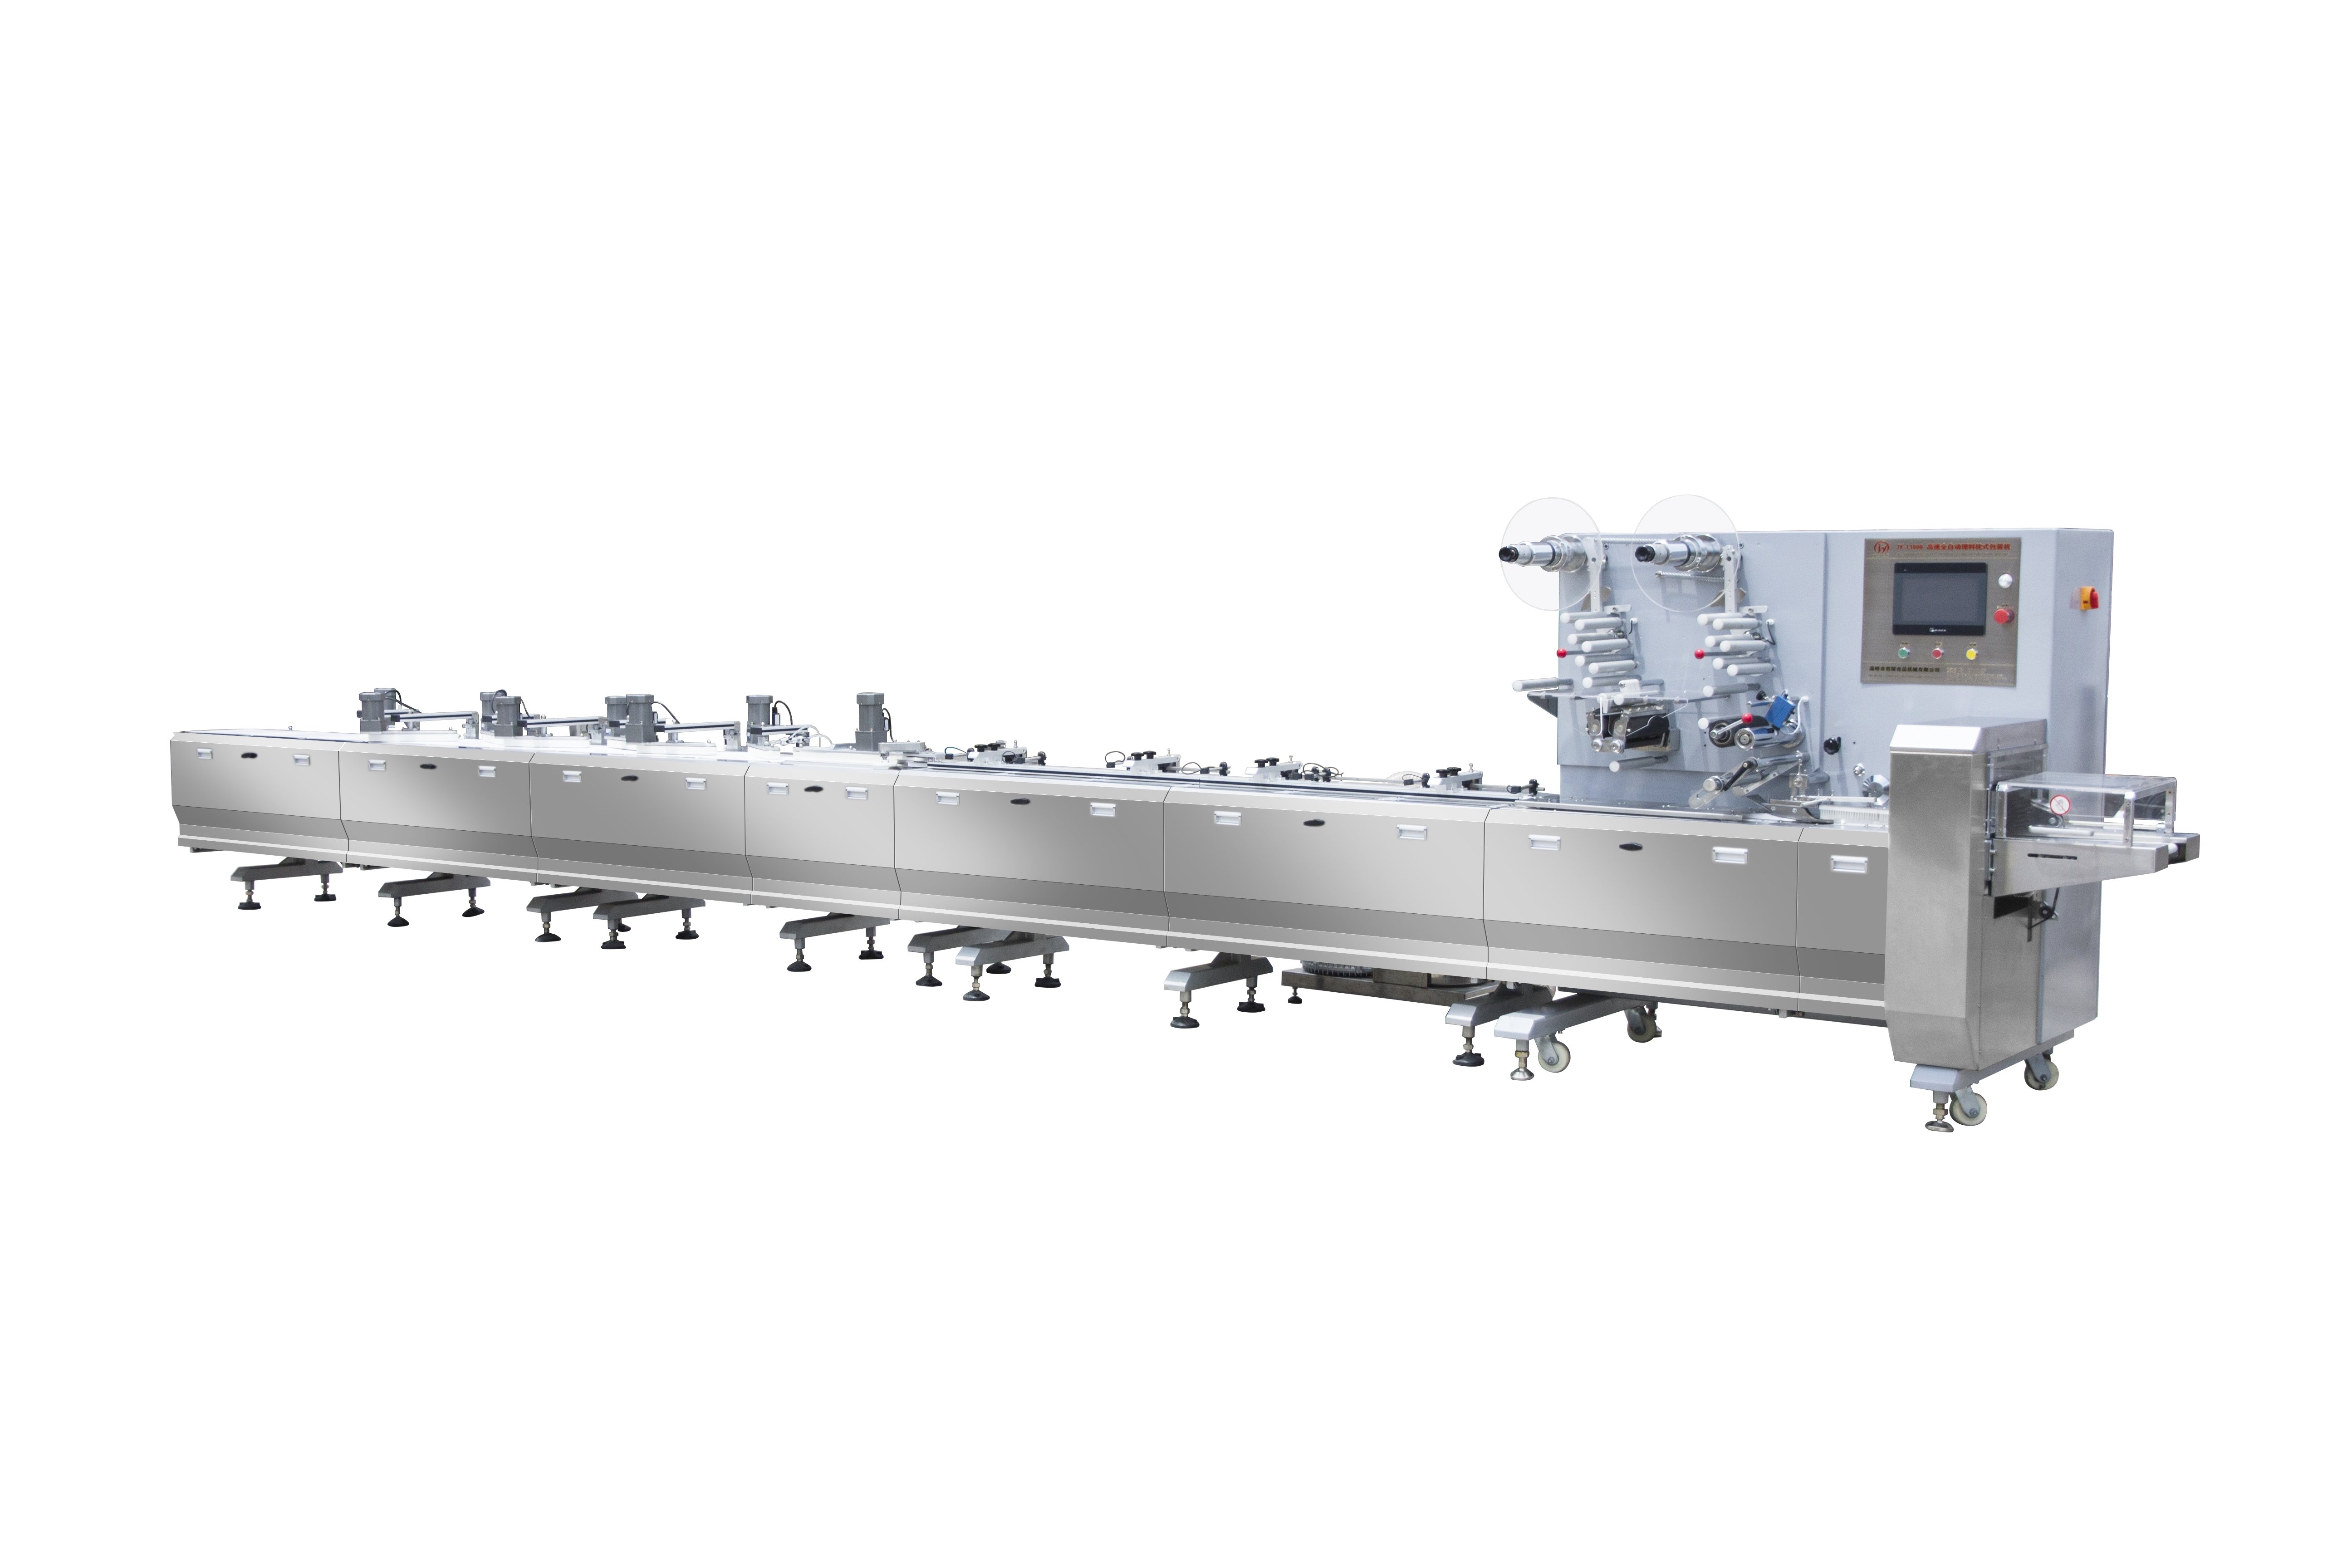
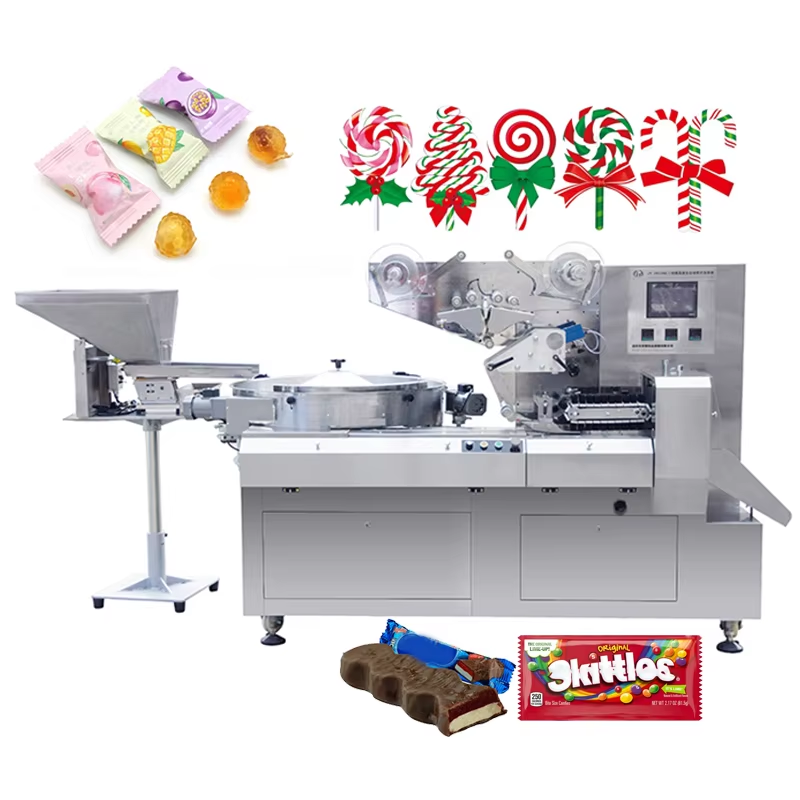
A food packaging machine supplier provides comprehensive solutions for businesses seeking to optimize their packaging operations. These suppliers specialize in delivering advanced machinery designed to automate the packaging process for various food products, from fresh produce to processed items. A professional food packaging machine supplier offers equipment that handles multiple packaging formats, including vacuum sealing, shrink wrapping, and automated container filling systems. The primary function of machinery from a food packaging machine supplier is to increase production efficiency while maintaining consistent quality standards. These machines are engineered to work with diverse packaging materials such as plastic films, paper, and flexible pouches, accommodating different product sizes and shapes. Technological features include precision sensors, programmable logic controllers, and automated quality control systems that ensure proper sealing and labeling. Applications for solutions provided by a food packaging machine supplier span across numerous sectors, including dairy, bakery, snacks, beverages, and ready-to-eat meals. The equipment protects products from contamination, extends shelf life, and maintains nutritional integrity during storage and transportation. Modern food packaging machine supplier offerings incorporate sustainable packaging options, reducing environmental impact while meeting regulatory compliance standards. Key technological advancements include servo-driven mechanisms for precise control, stainless steel construction for food safety compliance, and user-friendly interfaces enabling easy operation. A reputable food packaging machine supplier ensures their equipment meets international food safety certifications and hygiene standards, making them essential partners for food production facilities aiming to enhance operational performance.
New Product Releases

Choosing the right food packaging machine supplier delivers substantial operational benefits that directly impact your bottom line. First, efficiency gains are remarkable. These suppliers provide machinery that dramatically increases production capacity, allowing facilities to package significantly more products hourly compared to manual processes. This efficiency translates directly into reduced labor costs and higher output volumes. Second, quality consistency is guaranteed. A reliable food packaging machine supplier ensures every package meets identical standards regarding seal integrity, weight accuracy, and appearance. This consistency builds consumer trust and reduces product returns due to packaging defects, protecting your brand reputation. Third, cost reduction is substantial. While initial investment appears significant, the machinery from a quality food packaging machine supplier reduces waste, minimizes material consumption through optimized sealing, and decreases labor requirements. These factors combine to lower per-unit packaging costs considerably over time. Fourth, operational flexibility matters greatly. Modern equipment from a food packaging machine supplier accommodates various package sizes, shapes, and materials without requiring extensive reconfiguration. This adaptability enables businesses to diversify product offerings without purchasing multiple machines. Fifth, regulatory compliance is streamlined. A professional food packaging machine supplier ensures equipment meets all food safety standards, hygiene requirements, and labeling regulations, eliminating compliance headaches. Safety features protect both products and workers throughout the packaging process. Sixth, maintenance simplicity reduces downtime. Equipment from established food packaging machine suppliers includes comprehensive support, readily available spare parts, and detailed training programs. Quick access to service minimizes production interruptions. Finally, sustainability advantages align with modern consumer preferences. Advanced equipment reduces packaging material waste and energy consumption, supporting environmental goals while appealing to eco-conscious customers and improving corporate responsibility metrics.

Tips And Tricks

Why Soft Candy Wrapping Machines Are Key to Maintaining Product Quality

01

Jun

Why Soft Candy Wrapping Machines Are Key to Maintaining Product Quality

Soft candy is one of the most delicate confectionery products on the market. Its moisture content, texture, and shape make it highly vulnerable to environmental damage, mechanical stress, and improper handling. A reliable candy packaging machine is n...
View More
How Automatic Flow Pack Machines Reduce Labor Costs and Material Waste

22

Jun

How Automatic Flow Pack Machines Reduce Labor Costs and Material Waste

In high-volume production environments, packaging efficiency directly shapes profitability. A flow packing machine addresses two of the most persistent cost drivers in packaging operations: excessive manual labor and unnecessary material consumption....
View More
How Flow Packing Machines Improve Speed and Accuracy in Packaging

01

Jul

How Flow Packing Machines Improve Speed and Accuracy in Packaging

In today's competitive manufacturing environment, packaging speed and accuracy are no longer optional advantages — they are baseline requirements. A flow packing machine addresses both demands simultaneously, allowing production facilities to s...
View More
How Flow Packing Machines Transform Efficiency in Confectionery and Snack Packaging

29

Sep

How Flow Packing Machines Transform Efficiency in Confectionery and Snack Packaging

The confectionery and snack packaging industry demands precision, speed, and reliability to remain competitive in today's fast-paced market. A flow packing machine represents one of the most transformative technologies available to manufacturers seek...
View More

Get a Free Quote

Our representative will contact you soon.
Name
Email
Required Product
Message
0/1000

food packaging machine supplier

Advanced Automation Technology

Advanced Automation Technology

A leading food packaging machine supplier incorporates cutting-edge automation technology that revolutionizes production capabilities. The machinery features intelligent sensors and real-time monitoring systems that detect inconsistencies immediately, ensuring every package meets strict quality standards. Programmable automation allows customization for different product types without manual intervention between batches. This technological sophistication enables continuous operation with minimal human oversight, dramatically improving throughput. The food packaging machine supplier integrates touch-screen controls and data logging capabilities, providing operators with comprehensive performance metrics. Advanced servo motors deliver precise positioning and sealing, critical for maintaining product integrity. Integration with existing production systems simplifies implementation, and the food packaging machine supplier provides comprehensive technical support throughout installation and operation phases.
Cost-Effective Production Solutions

Cost-Effective Production Solutions

Investing in equipment from a reputable food packaging machine supplier yields impressive return on investment through multiple cost-saving mechanisms. The machinery minimizes packaging material waste through optimized sealing techniques and precise portion control. Energy-efficient motors and hydraulic systems reduce operational expenses significantly. A quality food packaging machine supplier designs equipment that operates continuously with minimal maintenance interruptions, maximizing productive hours annually. Labor costs decrease substantially as the food packaging machine supplier's automated systems handle tasks previously requiring multiple workers. Reduced packaging defects mean fewer product rejections and waste write-offs. The supplier typically offers flexible financing options and scaling solutions, allowing businesses to expand capabilities gradually. Long-term spare parts availability from the food packaging machine supplier ensures continued operation without expensive equipment replacement, protecting your initial investment effectively.
Compliance and Food Safety Standards

Compliance and Food Safety Standards

A professional food packaging machine supplier prioritizes food safety compliance above all other considerations. Equipment construction uses food-grade stainless steel throughout contact surfaces, preventing contamination and simplifying sanitation procedures. The food packaging machine supplier ensures all machinery meets FDA, HACCP, and international food safety certifications, eliminating regulatory uncertainty. Hygienic design principles prevent bacterial growth and product contamination risks. Advanced sealing mechanisms create airtight packages that extend shelf life while maintaining nutritional quality. The food packaging machine supplier provides detailed documentation confirming compliance with local and international regulations. Their equipment features modular components that withstand frequent cleaning without performance degradation. Traceability systems track packaging batches automatically, supporting rapid recall procedures if necessary. Professional support from the food packaging machine supplier includes regular compliance audits and updates to accommodate changing regulations, ensuring your facility maintains certifications continuously.
Newsletter
Please Leave A Message With Us