packing machinery
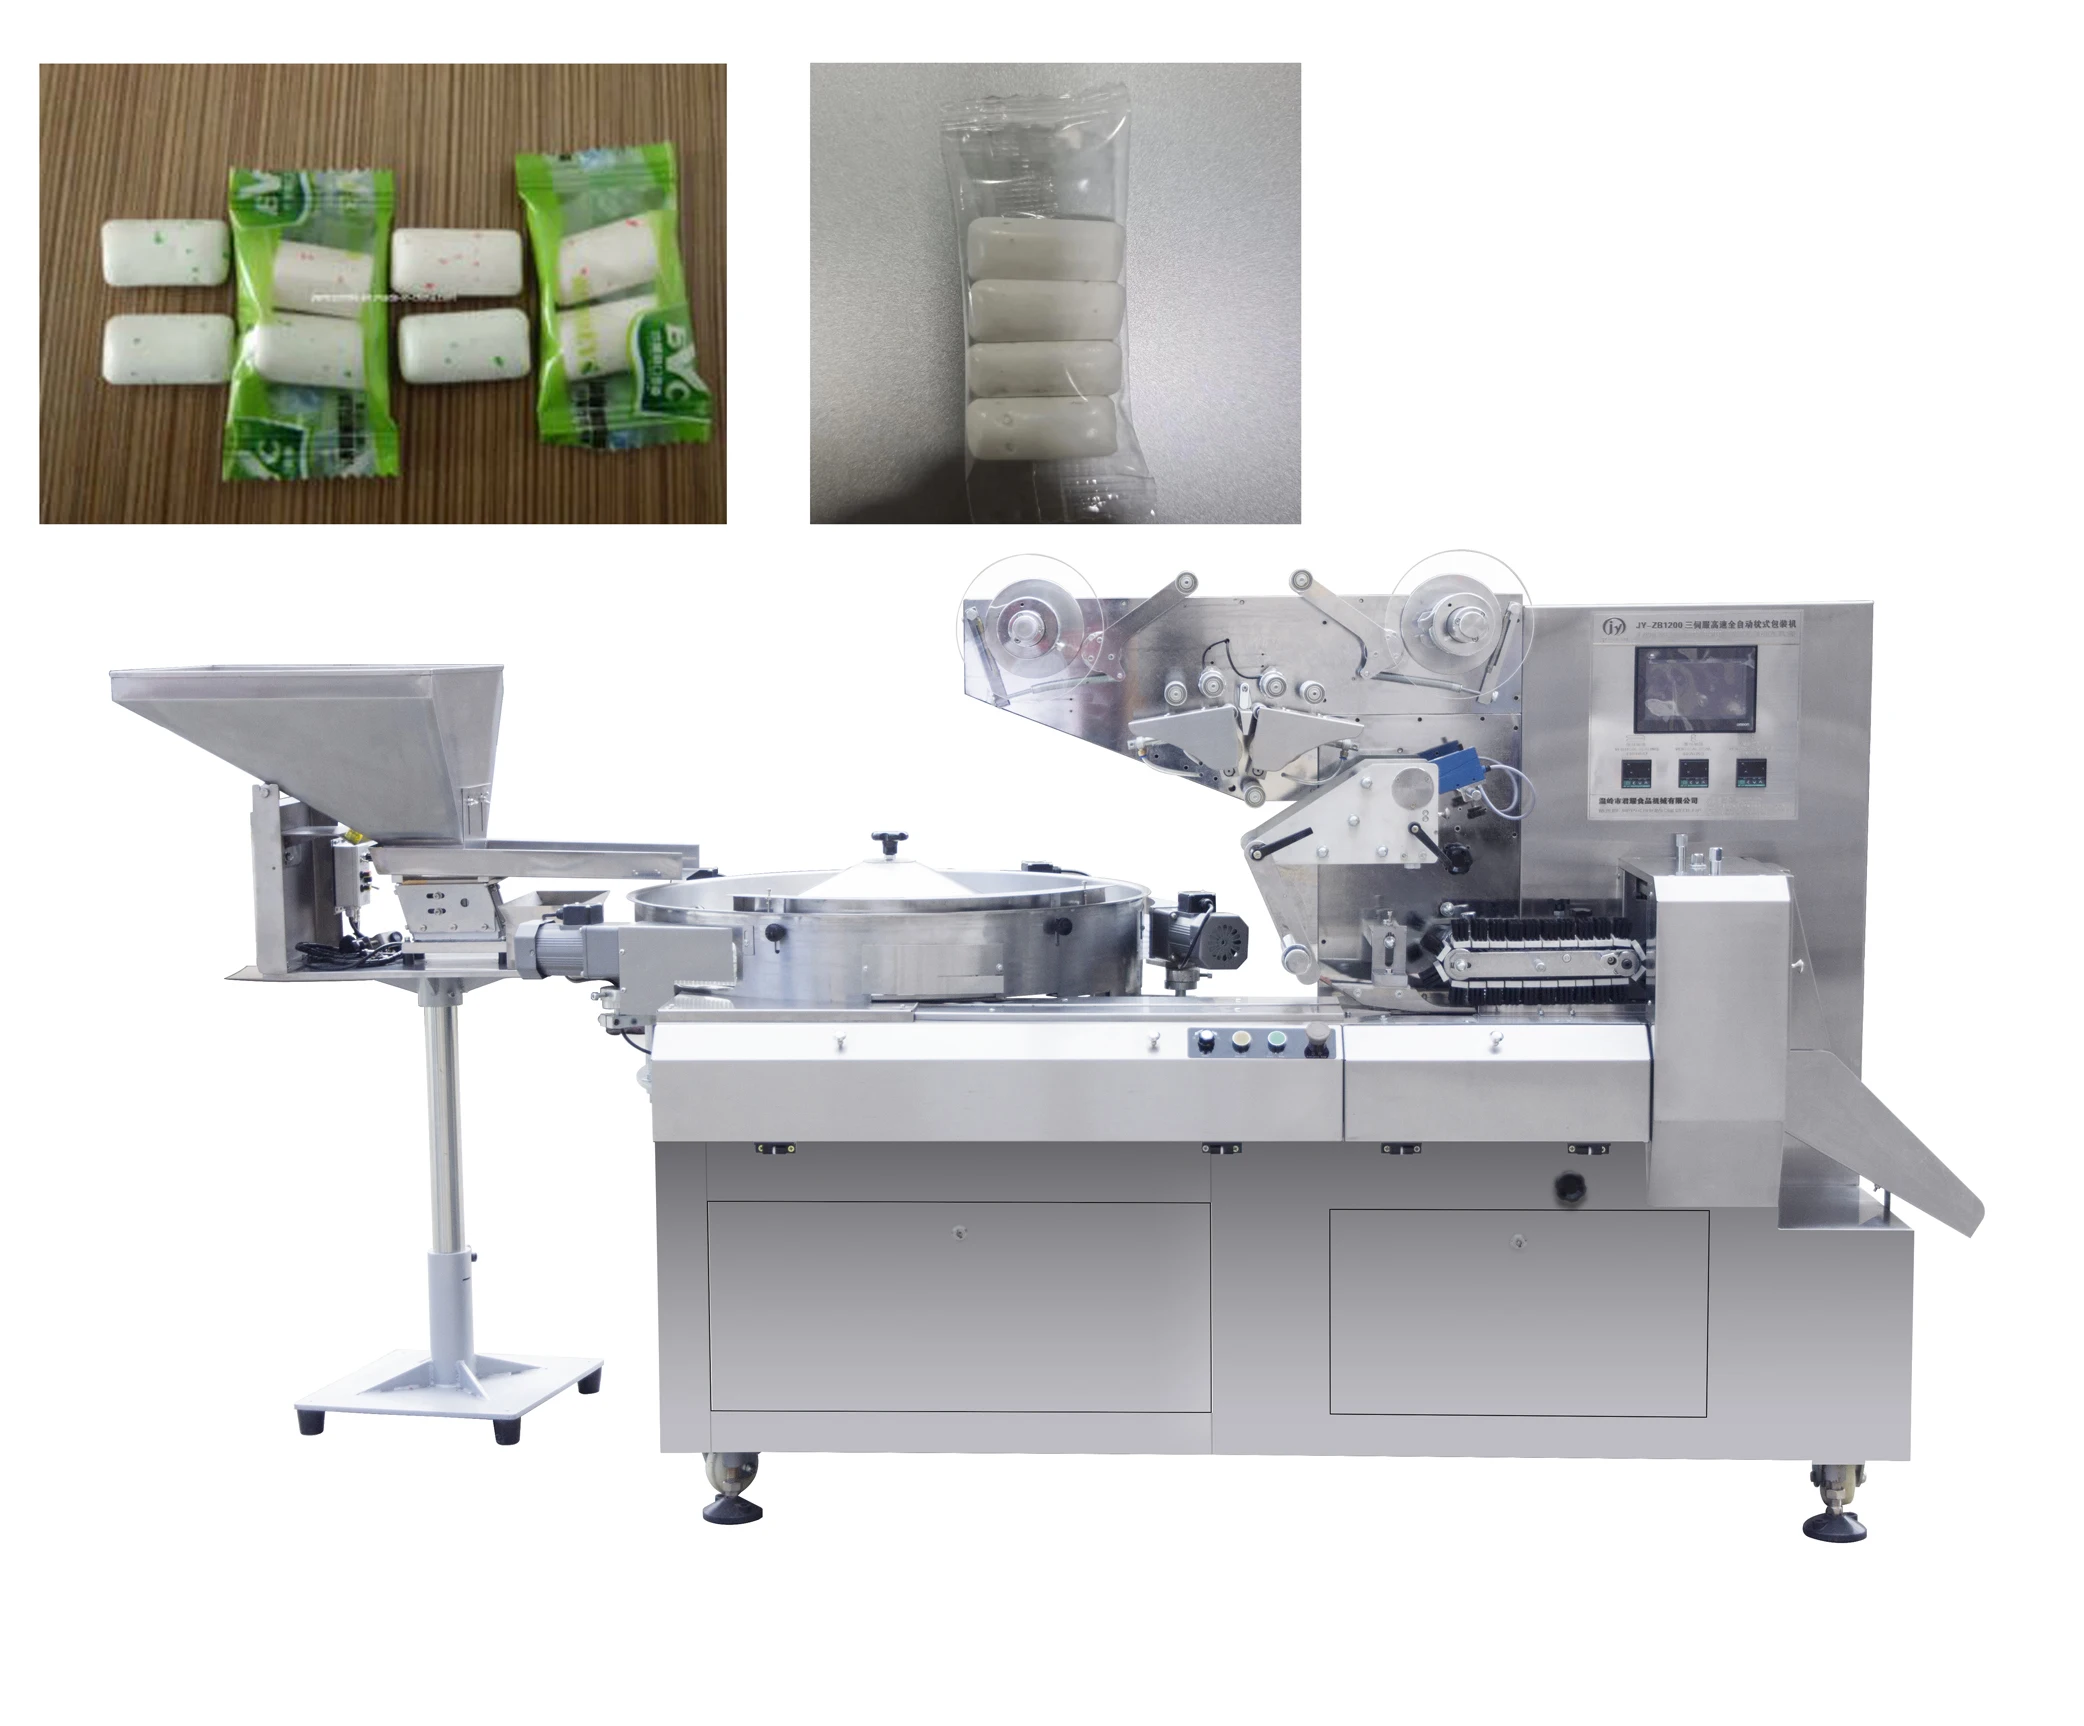
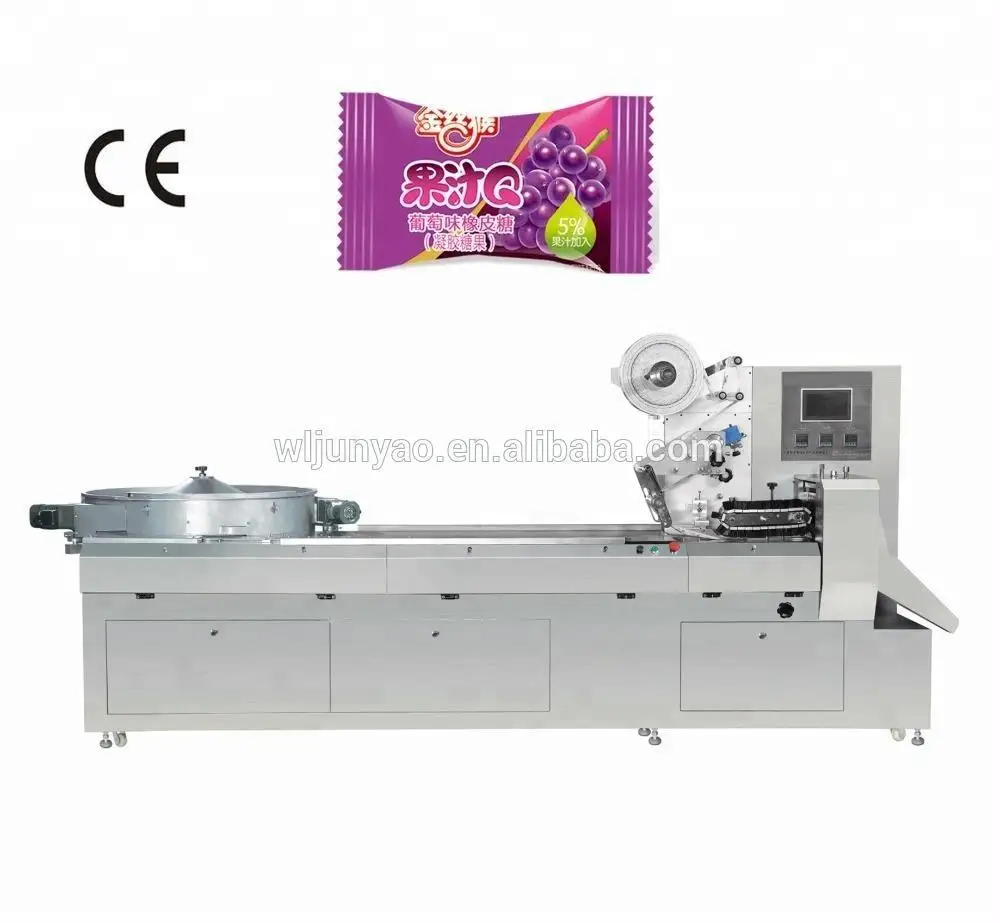
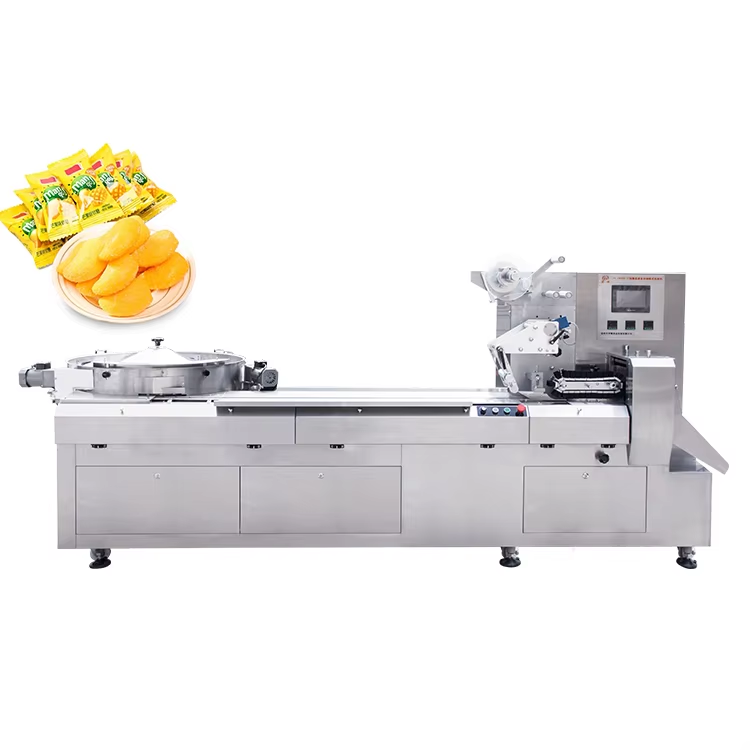
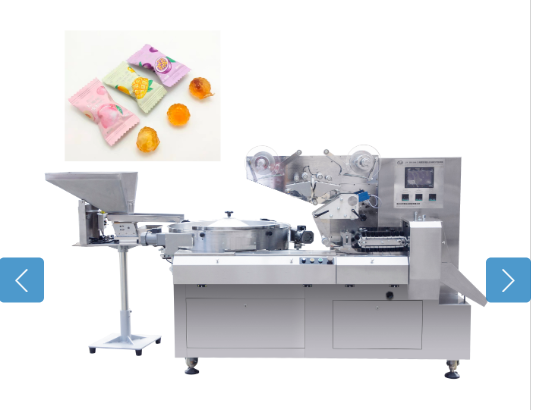
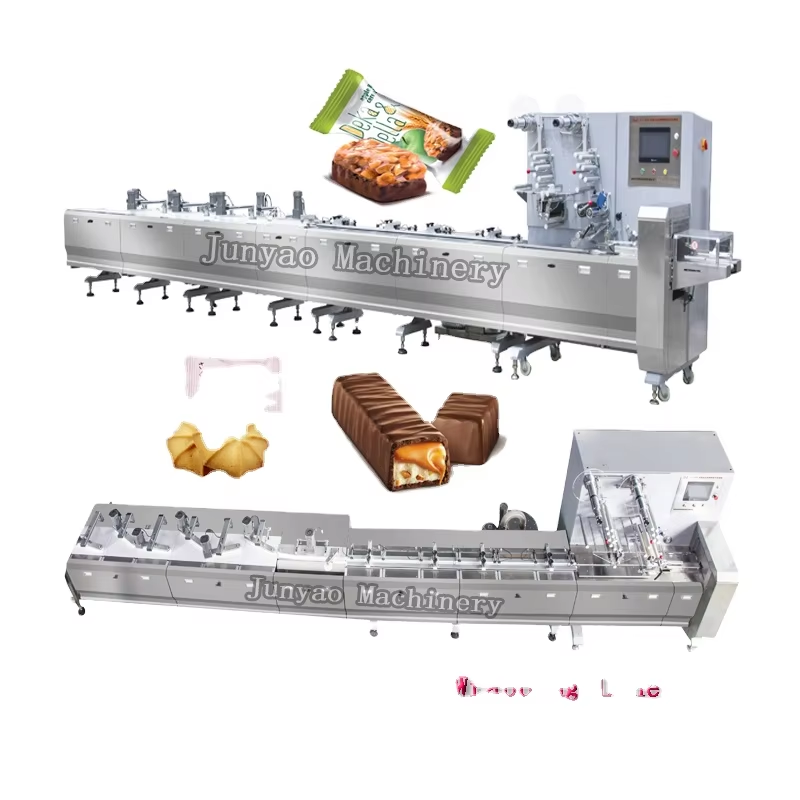
Packing machinery represents a critical investment for businesses seeking to streamline their packaging operations and enhance productivity. Modern packing machinery automates the entire packaging process, from product preparation through final sealing and labeling, significantly reducing manual labor and human error. These systems are engineered with advanced technological features designed to handle various product types, including liquids, powders, solids, and fragile items with precision and consistency.
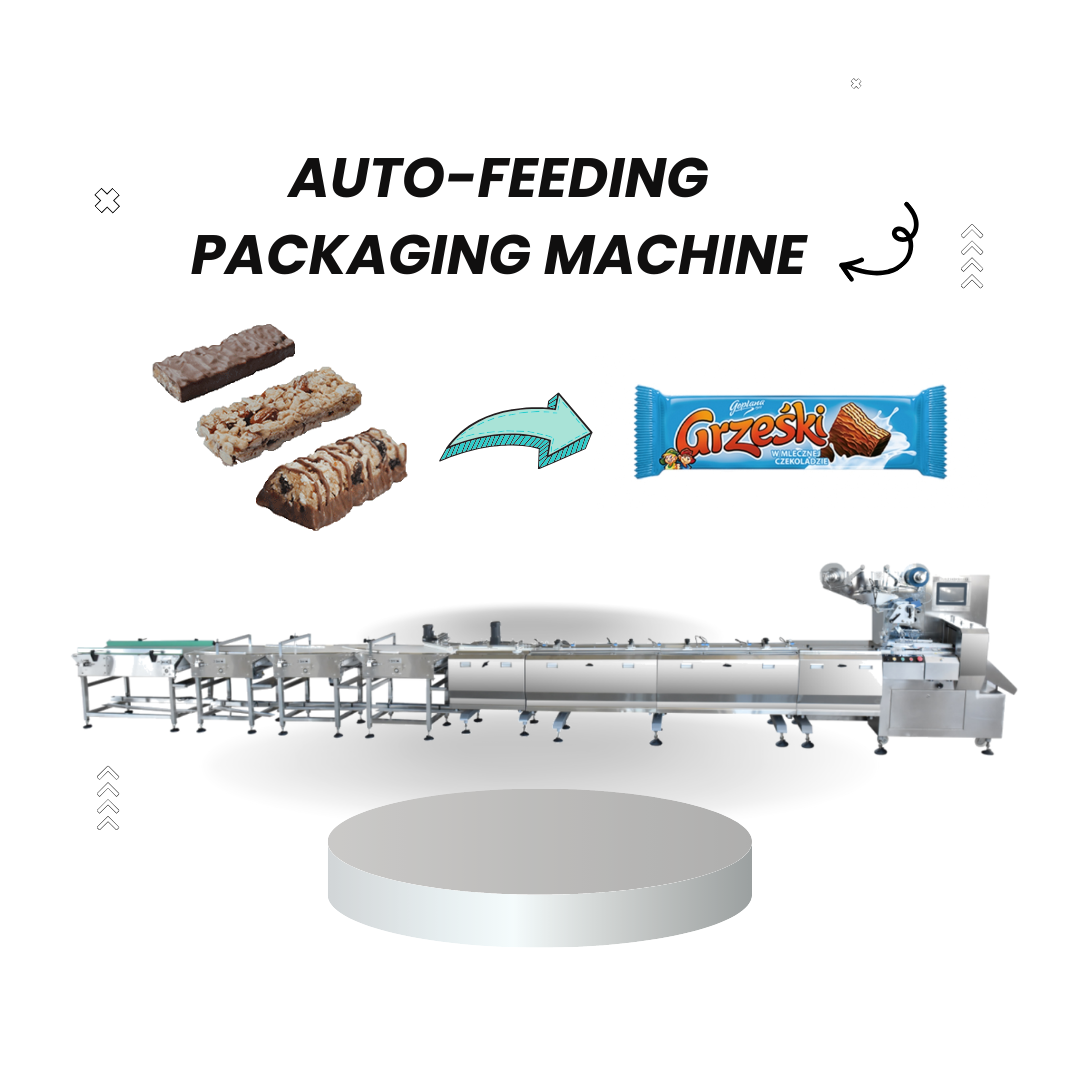
The core functions of packing machinery include product feeding, weighing, filling, sealing, coding, and labeling. Contemporary packing machinery incorporates servo motors, programmable logic controllers, and touchscreen interfaces that enable operators to customize settings for different products seamlessly. High-speed capabilities allow packing machinery to process hundreds of units per minute, substantially increasing output compared to traditional methods.
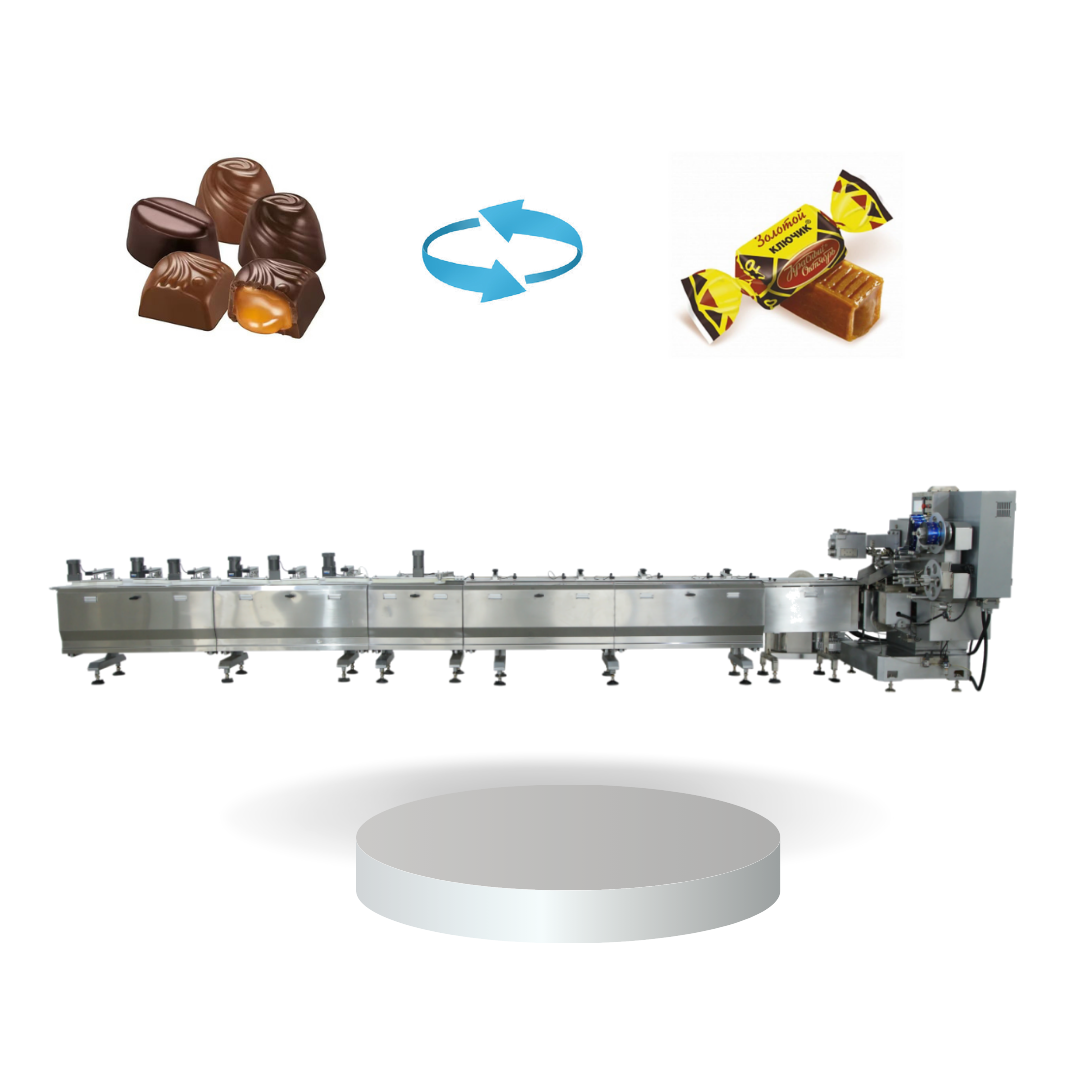
Applications of packing machinery span across multiple industries, including food and beverage, pharmaceuticals, cosmetics, and industrial goods. Whether packaging snacks, beverages, medical supplies, or household products, modern packing machinery adapts to diverse requirements. The integration of quality control sensors within packing machinery ensures every package meets strict standards before distribution, minimizing waste and protecting brand reputation.
Technological advancements have made packing machinery more user-friendly and efficient. Predictive maintenance systems monitor equipment performance, reducing unexpected downtime. The versatility of packing machinery makes it an essential component for companies aiming to scale operations while maintaining consistent quality standards across all packaged products.
 EN